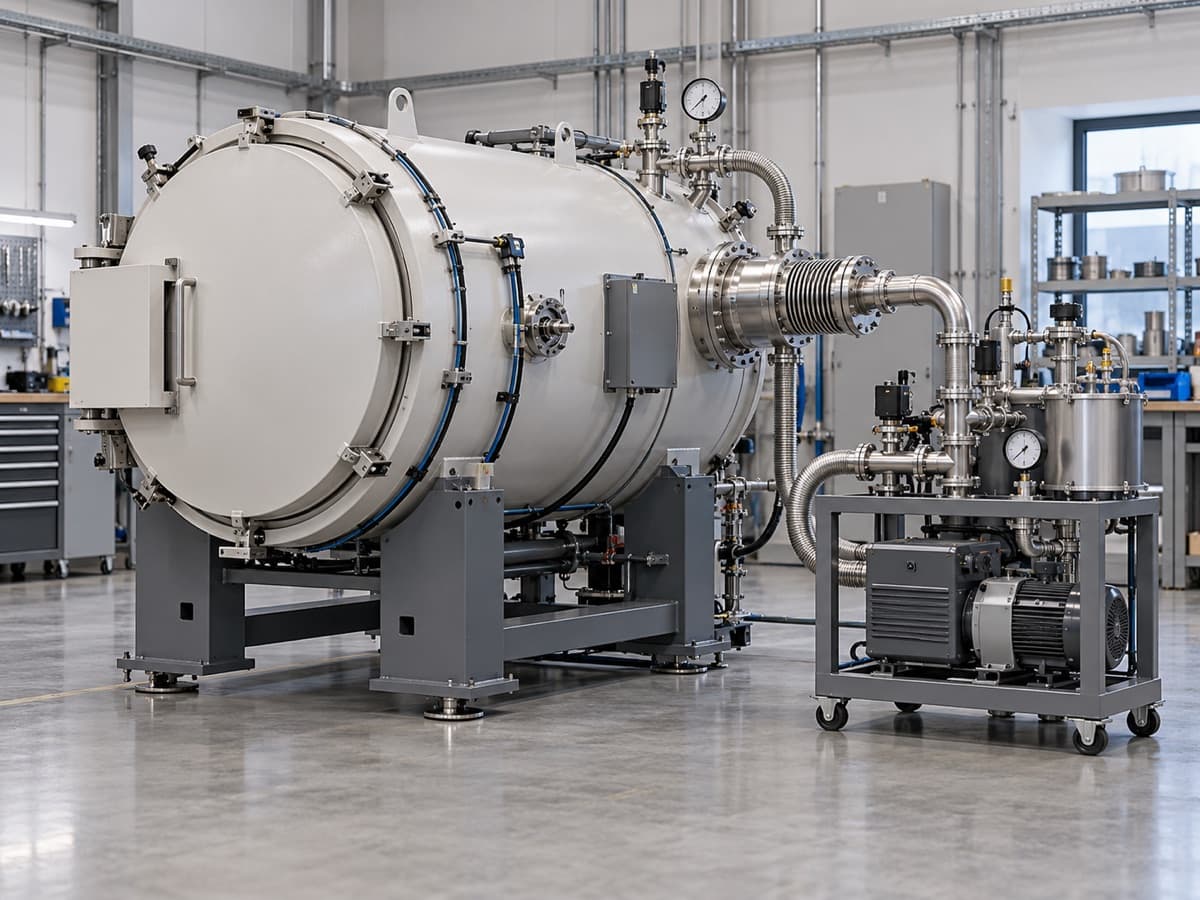
Sintering under vacuum removes the binder cleanly and eliminates the residual porosity that traps gas in an atmosphere furnace. For cemented carbide the result is a denser part with fewer pore defects; for technical ceramics it is a controlled grain structure at a repeatable density.
The hot zone is graphite felt insulated with graphite heating elements, giving ±5 °C uniformity across the working volume. Partial-pressure argon can be admitted during the binder removal and sintering stages, and an over-pressure sinter-HIP option consolidates the last percent of porosity in the same cycle.
Recipes are multi-segment with independent temperature, ramp rate, dwell and pressure per segment, stored by part number and logged per batch.