FL-IH-HRD
Induction Hardening Machine
Scan or single-shot hardening with servo traverse, integrated quench and closed-loop power control — repeatable case depth on shafts, gears and rails.
Read More →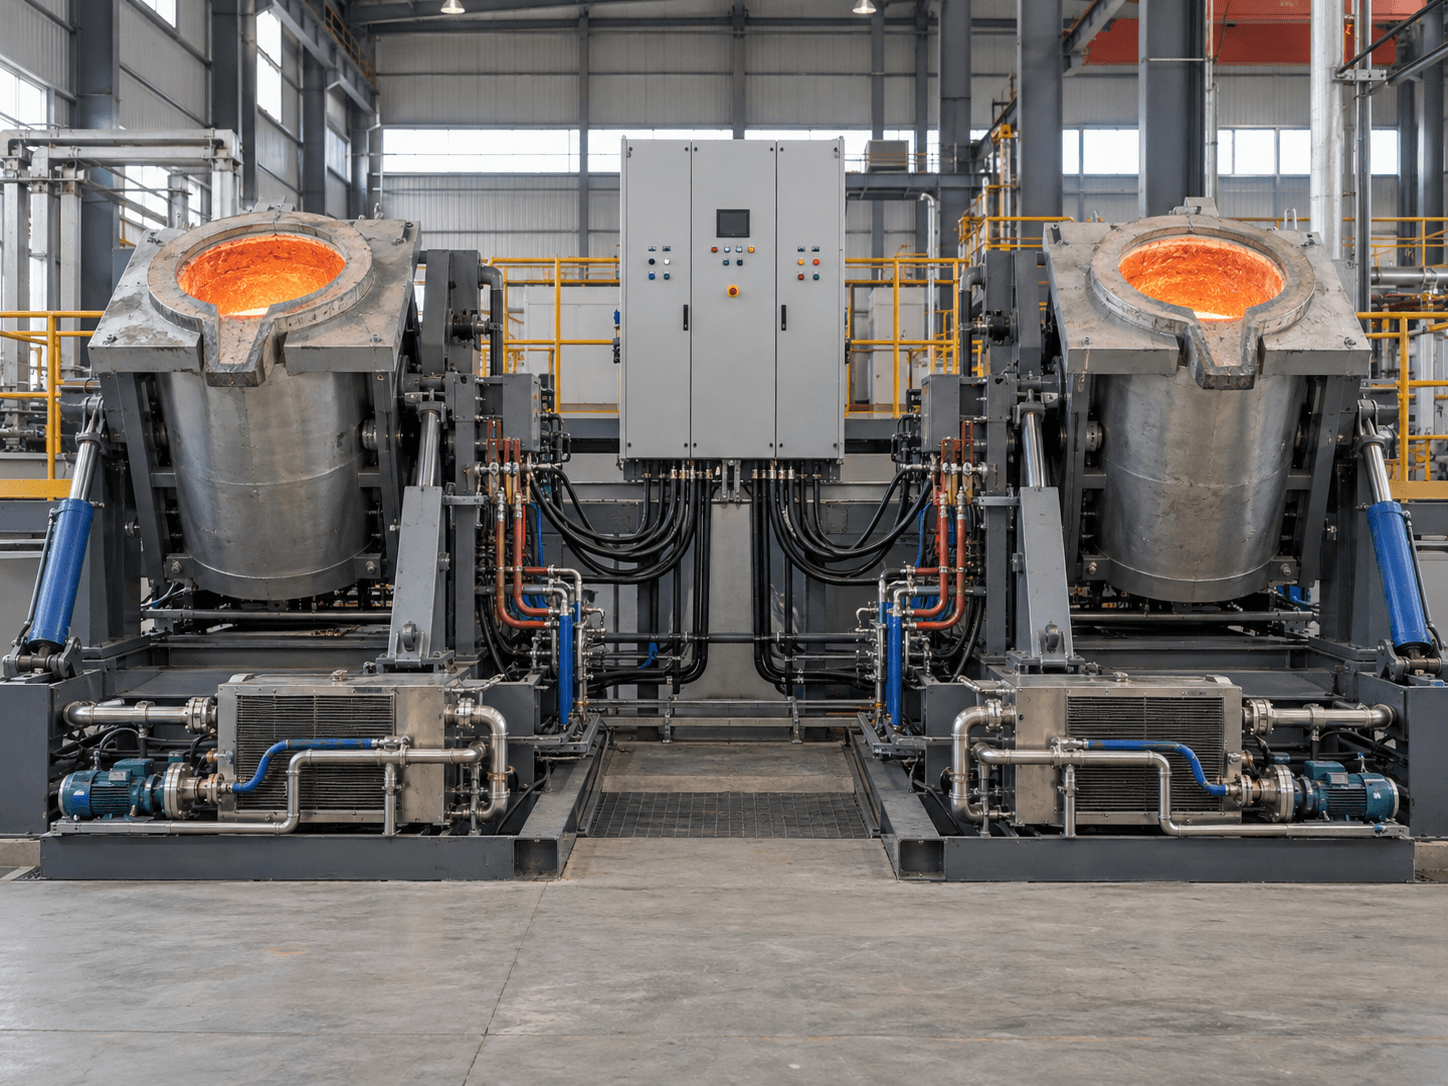
Induction heating manufacturer since 1998 · Built to your grid voltage · Installation & commissioning worldwide
Industry Application
Melting, forging heat and induction hardening with per-part data logging — built for automotive traceability and PPAP-level process control.
Automotive supply means proving the process, not just the part. Every heat, every billet and every hardened shaft has to be traceable to a set of recorded parameters, and an audit will ask for the data.
Our automotive installations log power, temperature, scan speed and quench conditions per part, exportable to your MES. Hardening recipes are stored by part number so a changeover cannot silently alter the case depth.
The three problems that decide whether an installation in this industry pays for itself or becomes a maintenance liability.
Per-part logging of every process variable, retained on the machine and exportable to your quality system, so an audit request is a file rather than a reconstruction.
Recipes are locked by part number and require an authorised login to change, which removes the operator adjustment that quietly drifts case depth over a production run.
Heating and hardening stations are specified to the line's takt time with margin, and the reject gate keeps an out-of-spec part from consuming a downstream station.
The configurations we most often specify for automotive components operations.
FL-IH-HRD
Scan or single-shot hardening with servo traverse, integrated quench and closed-loop power control — repeatable case depth on shafts, gears and rails.
Read More →FL-IH-BIL
GTR series through-heating line for round and square billets, with pyrometer control, hot and cold reject gates and press synchronisation.
Read More →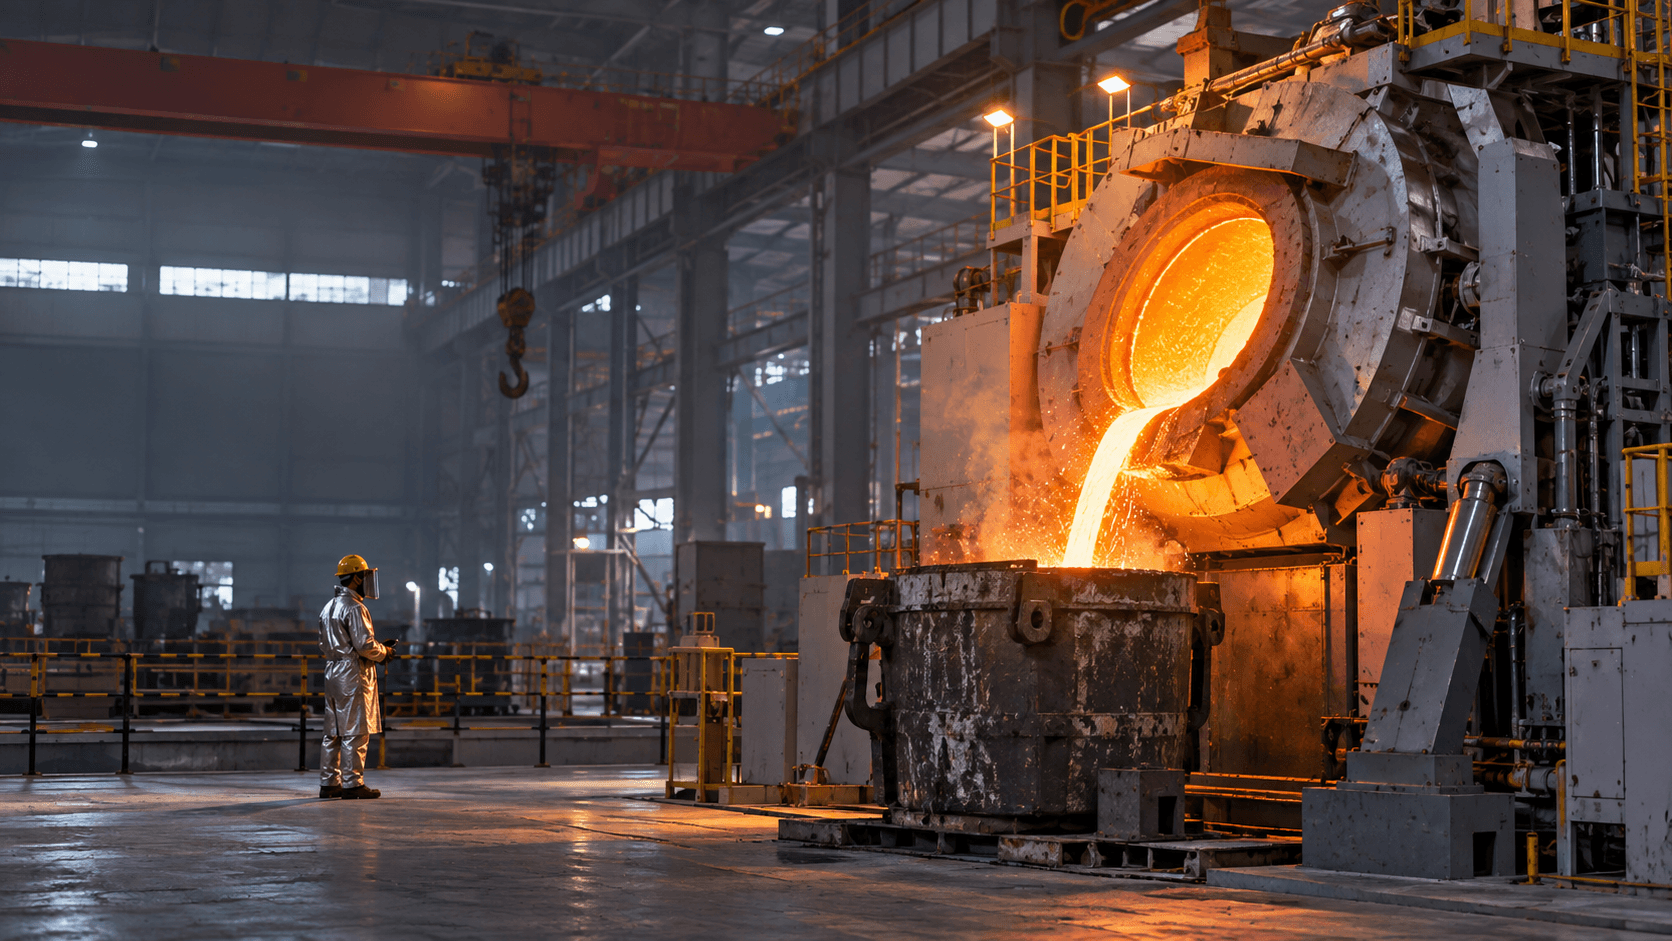
FL-GW-SS
Fully welded steel-shell furnace with magnetic yoke and hydraulic 95° tilting, from 0.5 to 5 tons per body — the standard choice for continuous foundry melting.
Read More →Coreless melting furnaces from 0.5 to 5 tons per body for grey iron, ductile iron, carbon and alloy steel castings, configured for continuous three-shift production.
Read MoreMelting plants for scrap processors converting mixed feed into saleable ingot or billet, with charge handling and fume extraction sized to the operation.
Read MoreThrough-heating and end-heating lines synchronised to your press, with automatic reject gates, quick coil changeover and low scale loss.
Read MoreSend your alloy, target output per hour, working hours and grid voltage. You will get a capacity recommendation, a plant layout and a firm quotation — normally within three working days, no obligation.