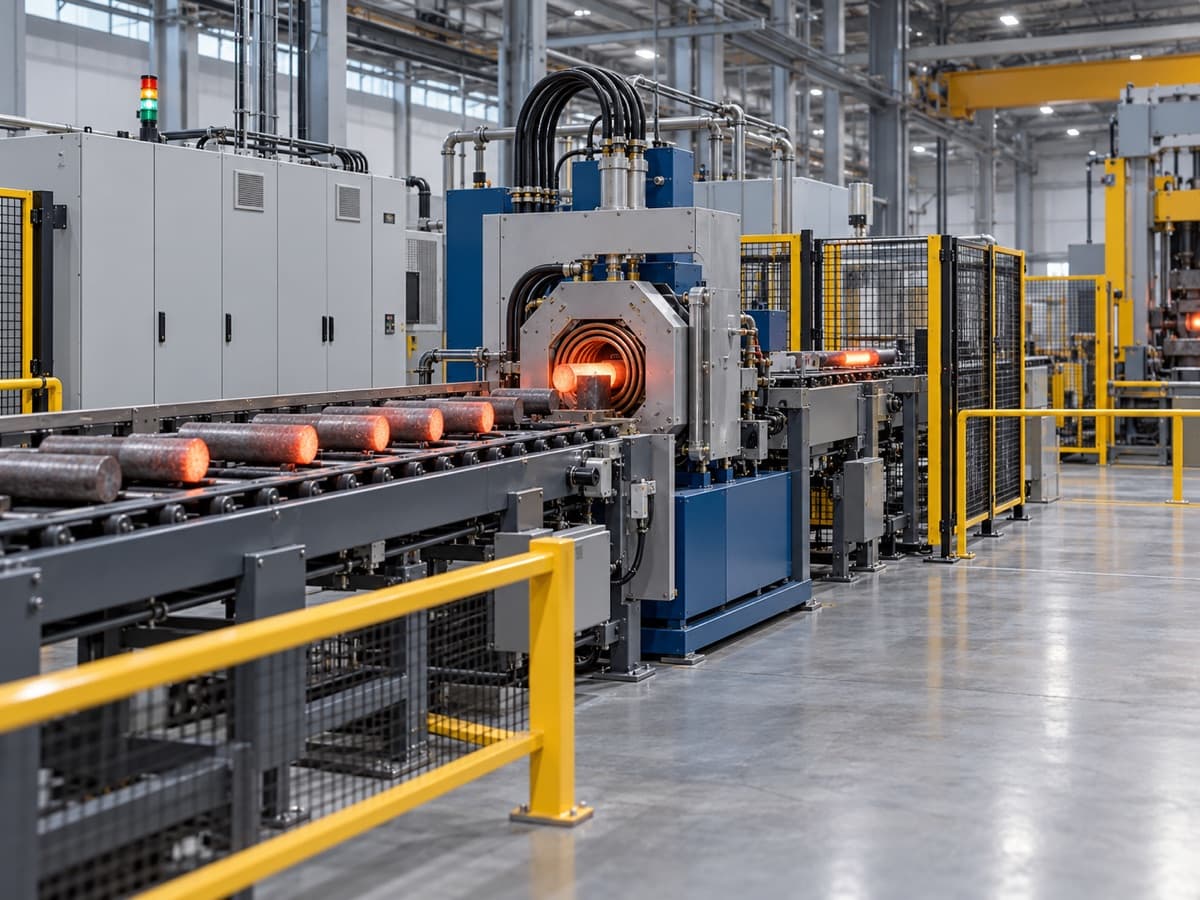
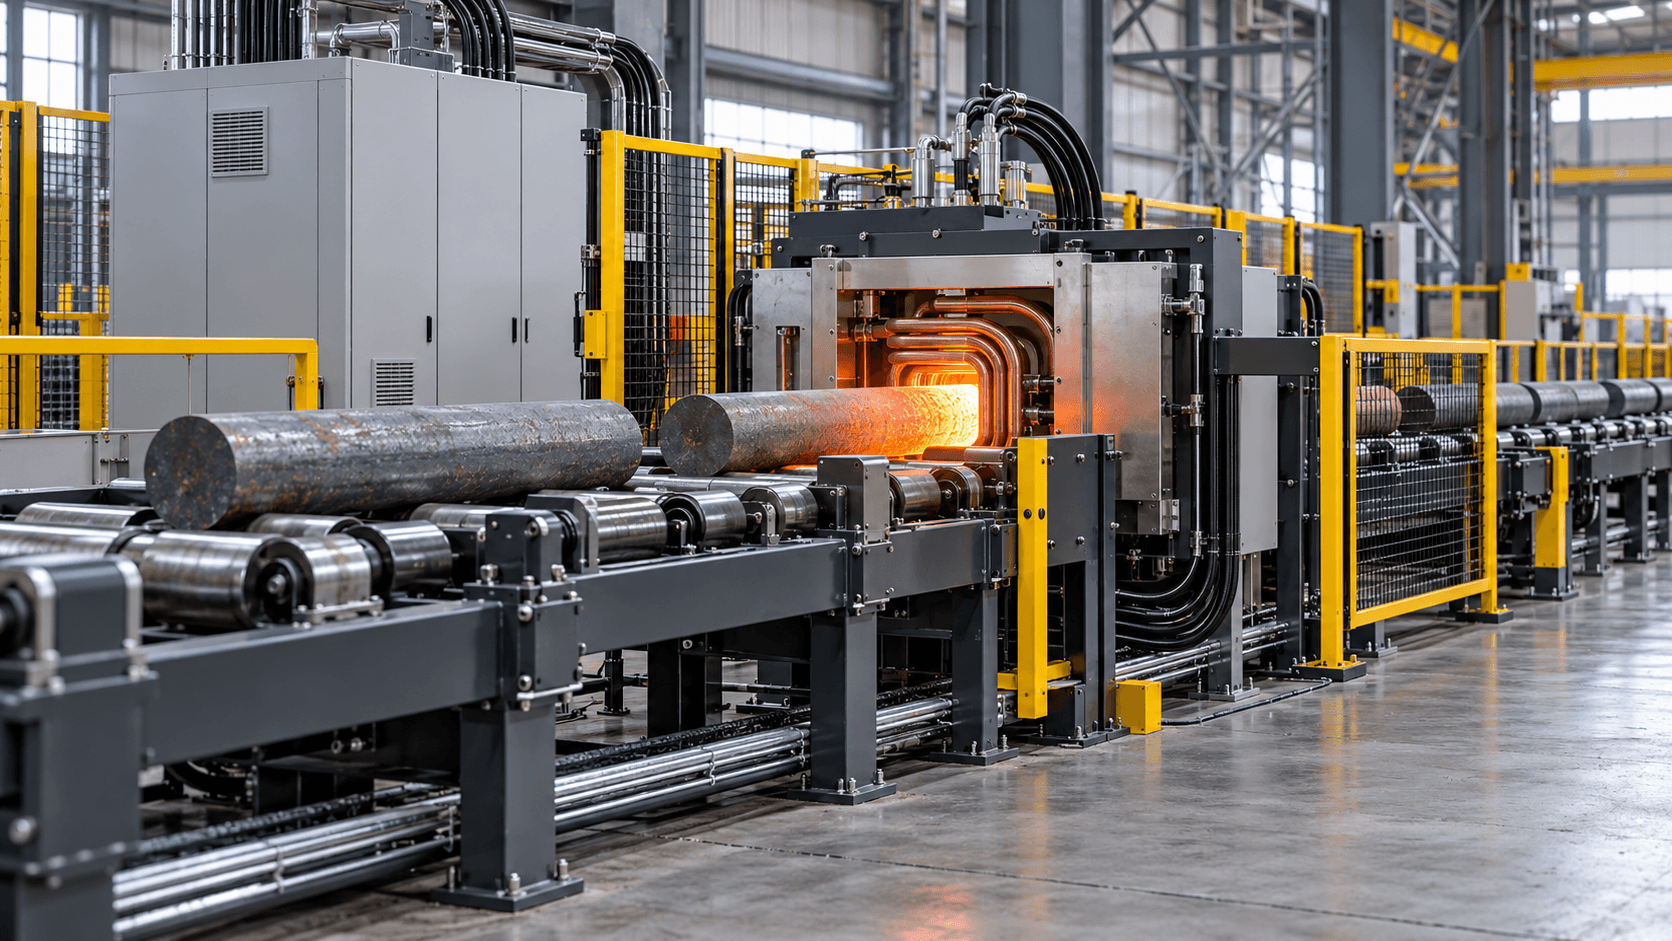
Induction heating puts energy where you want it: a billet reaches forging temperature in seconds rather than the tens of minutes a gas furnace needs, with far less scale loss and no furnace warm-up before the first shift.
We build three families — through-heating lines that bring a whole billet or bar to forging temperature, end-heating units that heat only the section being upset, and hardening machines that heat a surface layer for quench. All use closed-loop pyrometer control, so part temperature is a controlled variable rather than a consequence of dwell time.
Lines are supplied with the coil, power supply, feed and discharge handling, temperature control and reject gate. We match the coil to your part geometry — sending us the part drawing and the production rate is enough for us to quote a working line.