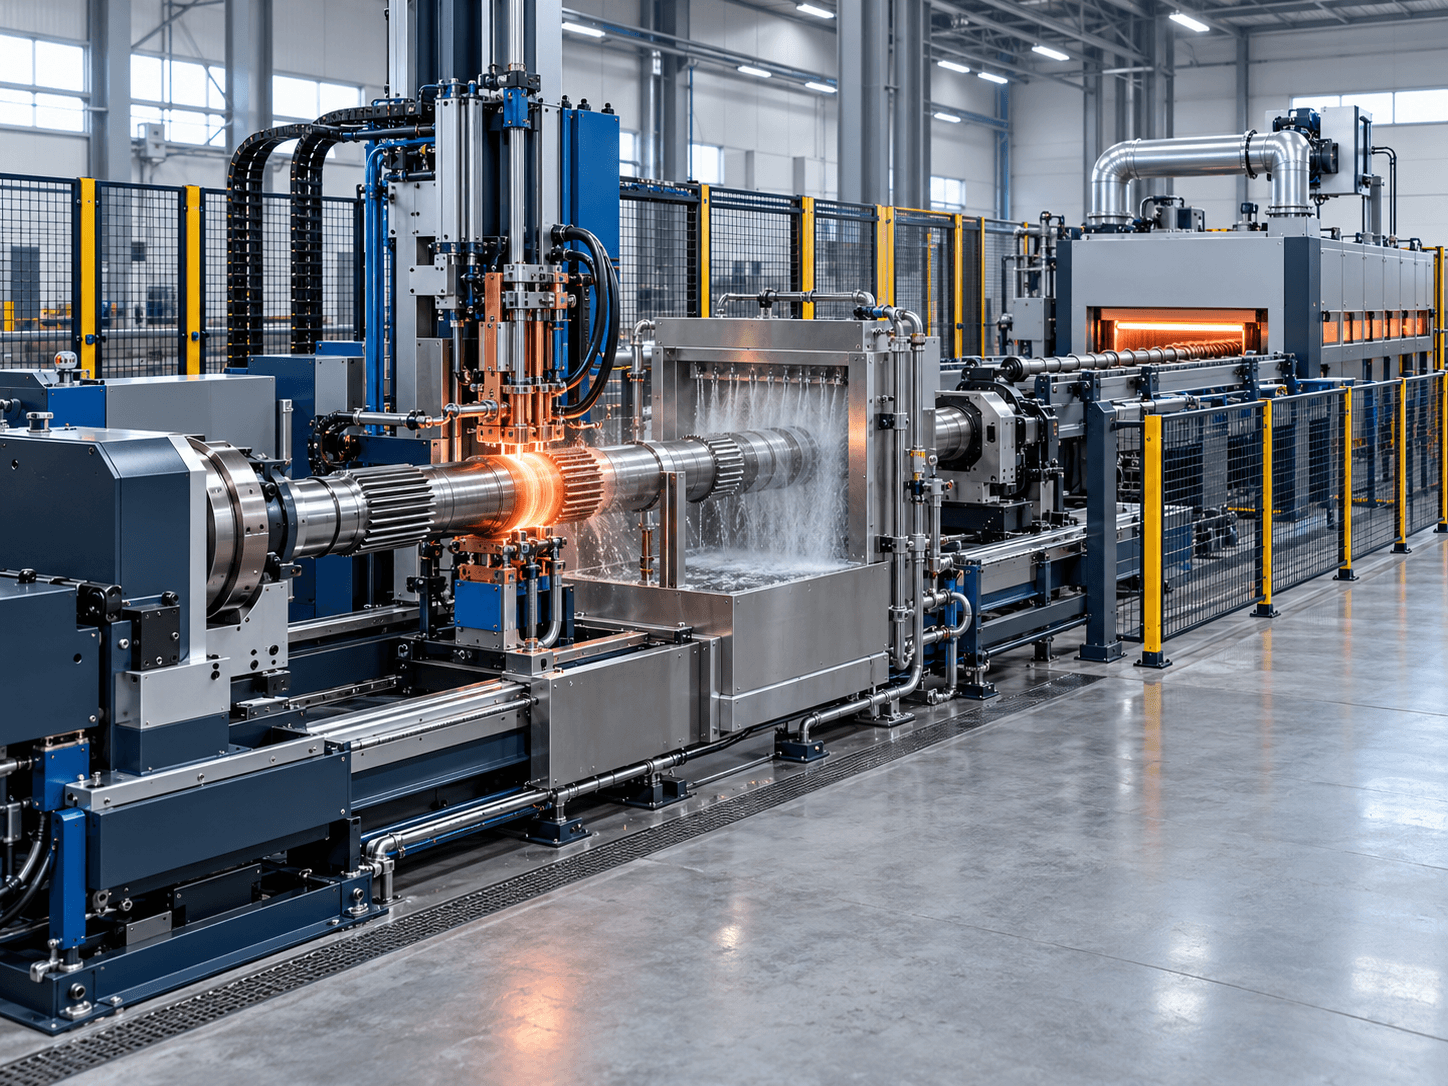
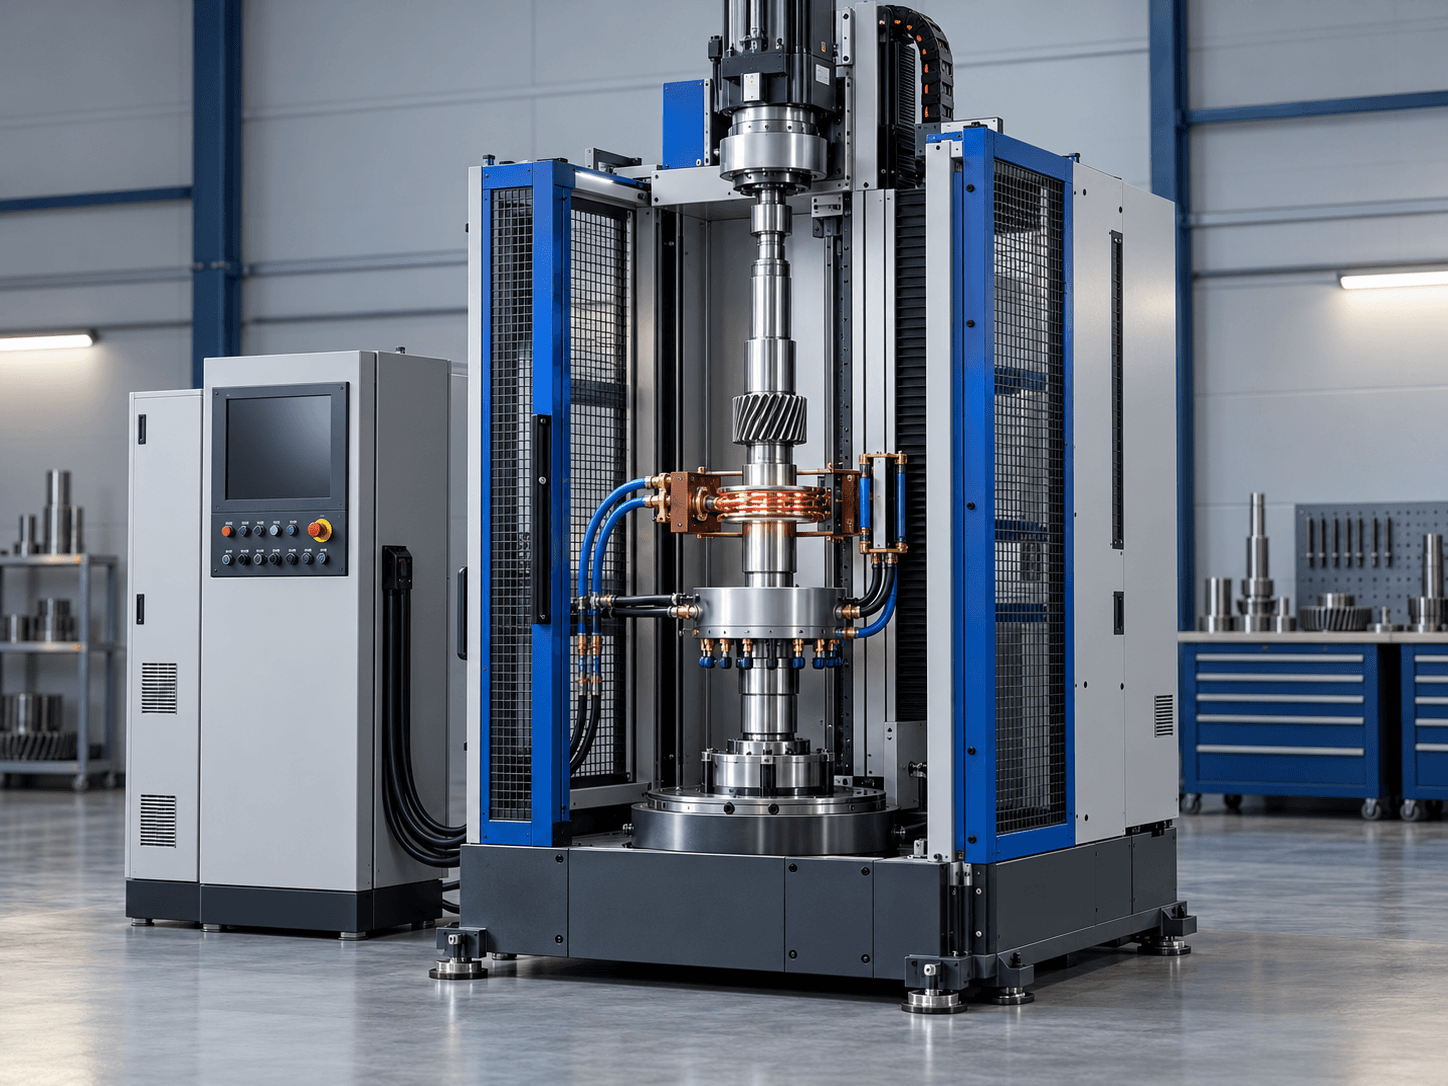
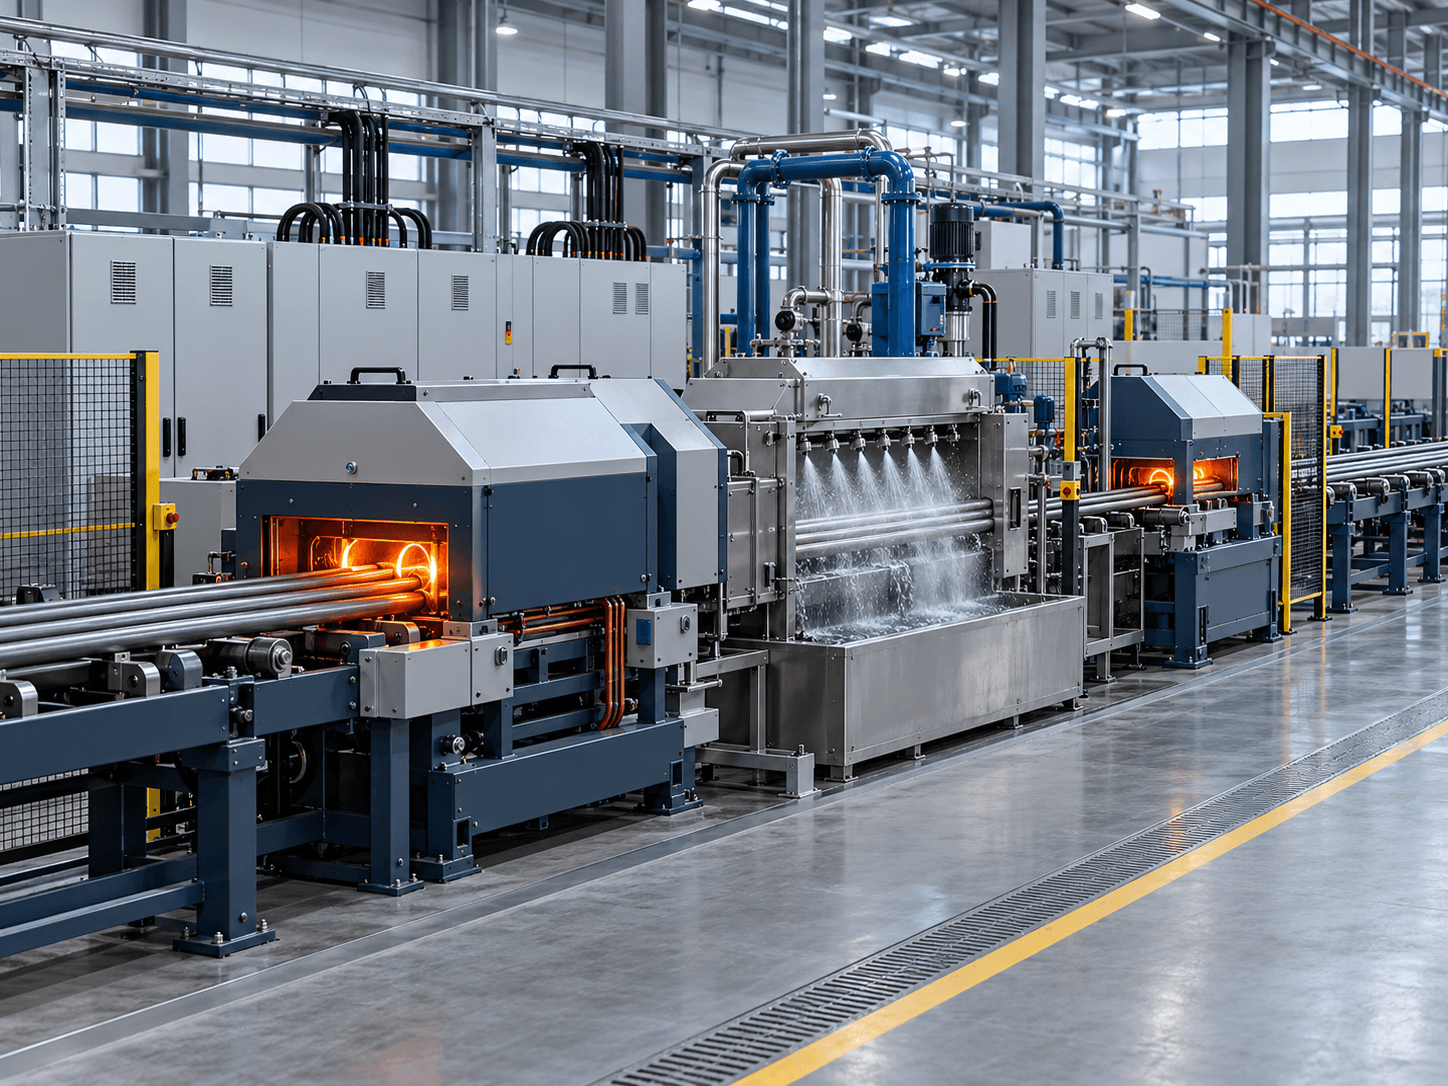
Choose a process route by workpiece and production need: scan or single-shot induction hardening for selected surfaces, or continuous quenching and tempering for bar, strand and tube. The equipment scope starts with the part and required metallurgical result, not a generic power rating.
For a useful engineering review, share the component drawing, material grade, treated zones, target hardness and case-depth requirement, output or takt time, and available utilities. Coil geometry, power/frequency, quench delivery, handling and any tempering stage are then reviewed as a system.
Process outcomes depend on the steel, geometry, coil and quench design, thermal cycle and acceptance method. Final values and validation scope are confirmed against the application and, where required, sample trials before equipment specification.