Skip to content
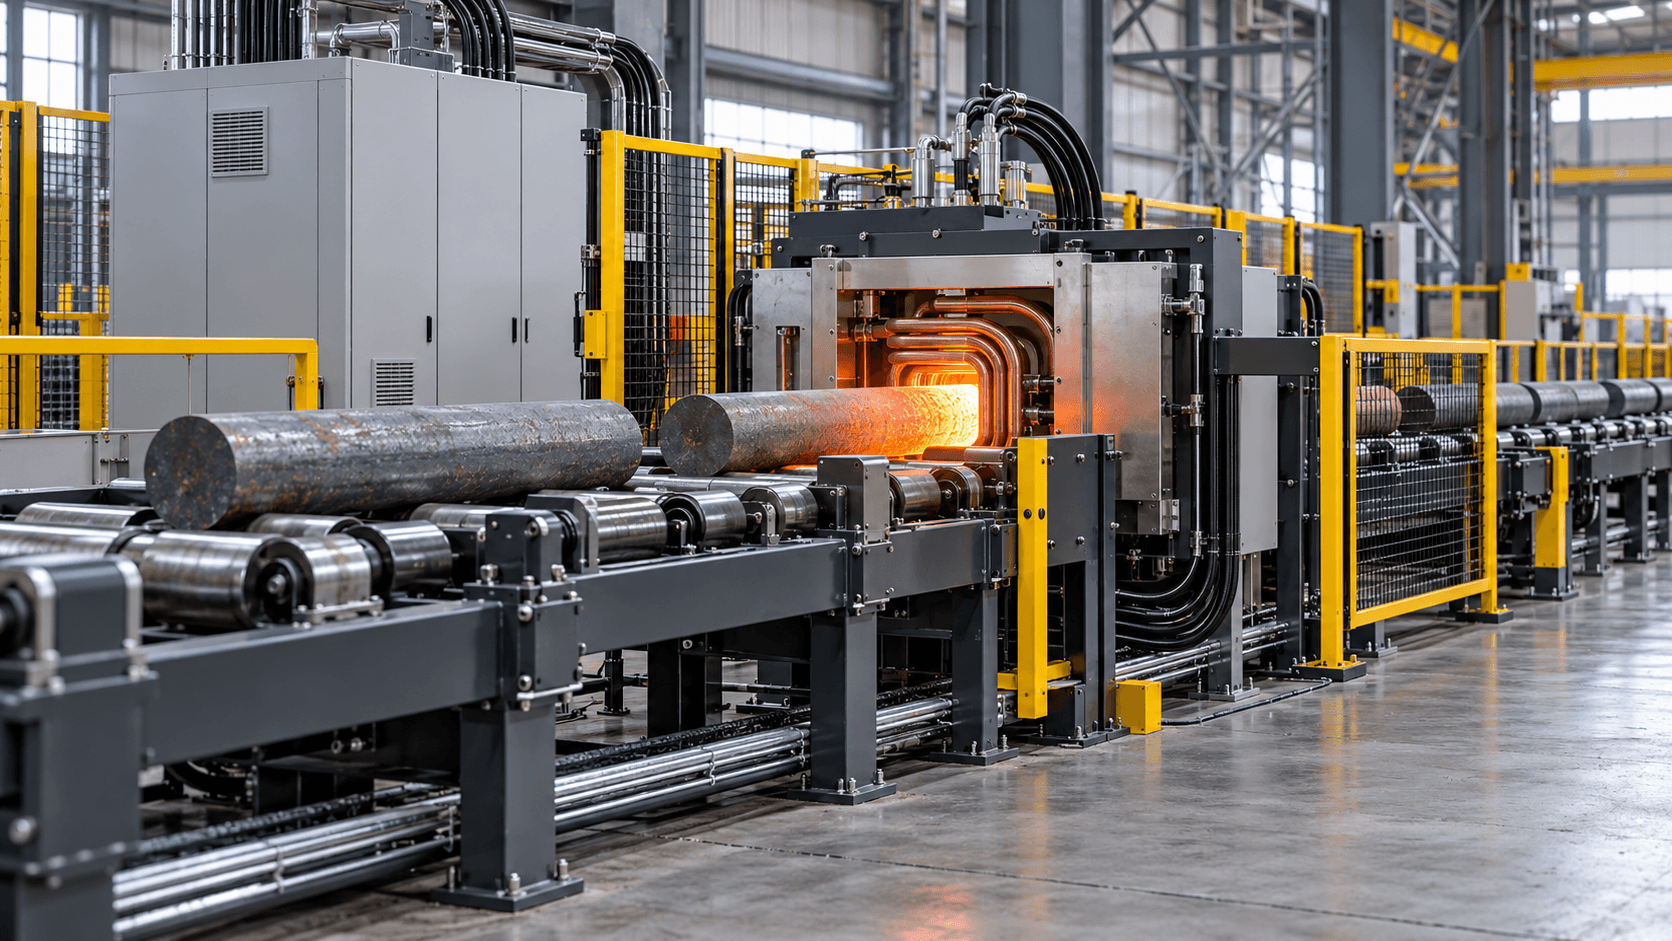
Induction billet heating line with steel bars moving through a guarded coil station

Illustrative product concept; final configuration and specifications are confirmed during engineering review.

Material & process

Share the workpiece alloy, dimensions and target process so the equipment route can be reviewed.

Output & duty

Define batch or throughput needs, operating schedule and required temperature or treatment result.

Site & utilities

Confirm available power, cooling, layout and destination-market requirements before final specification.

Induction Heating Systems · FL-IH-BIL

GTR Series Induction Billet Heating Furnace for Forging and Extrusion Lines

GTR series through-heating line for round and square billets, with pyrometer control, hot and cold reject gates and press synchronisation.

  • Through-heating or localized heating selected for the part geometry
  • Coil and power configuration reviewed against billet material and section
  • Temperature measurement and process window defined with the buyer
  • Feed, discharge and reject/diversion logic scoped to the production line
  • Press-side interface and operating sequence reviewed during layout planning
  • Optional recipe and energy-data requirements discussed in the project brief
Billet form and section
Round or square; dimensions reviewed from the buyer’s drawing
Material and grade
Confirmed from the workpiece specification
Target heating window
Set against the alloy and forging process during engineering review
Required output
Scoped to the press cycle, product mix and operating schedule
Temperature sensing
Selected for the process and acceptance requirements
Power and frequency
Configured to the workpiece, throughput and available utilities
Handling and controls
Feed, discharge and press interface confirmed to the plant layout
Final configuration
Confirmed after technical review; trials or acceptance checks scoped as needed

Product Details

A billet induction heating line is specified around the workpiece alloy, cross-section, length, target heating window and the forging process. Coil geometry, power and sensing strategy are reviewed against those inputs rather than assumed from a generic catalogue model.

The proposed line layout may include feed and discharge handling, temperature sensing, control, diversion logic and a press interface. The handling method and automation scope are confirmed against the plant layout, product mix and operating sequence.

To assess the process route, share billet drawings, material grades, required output, press-cycle information and available electrical and cooling utilities. The engineering review then defines which configuration and acceptance checks are appropriate.
FL-IH-END

Bar End Heating Machine

Heats only the section to be formed — hand tools, axles, anchor bolts and eye bolts — cutting energy per part sharply versus full-length heating.

Read More →
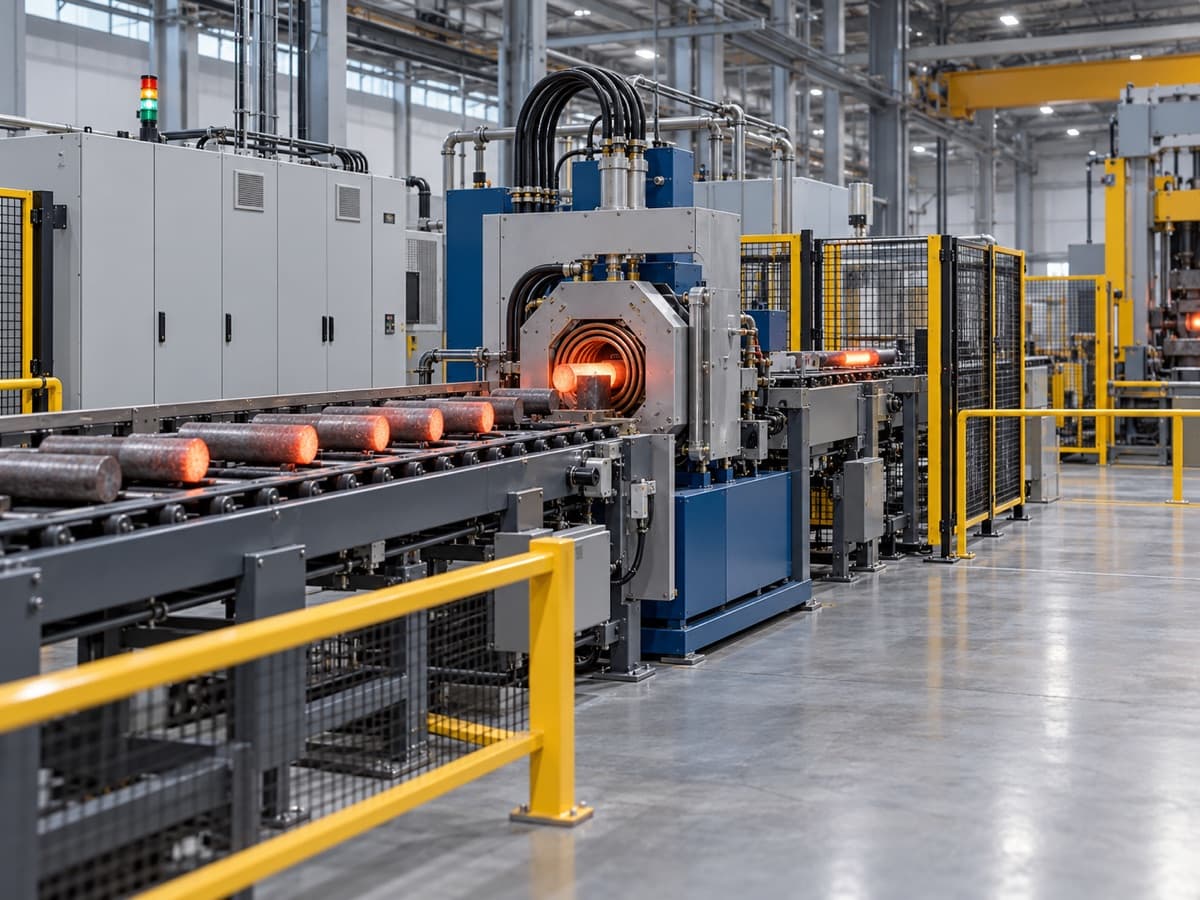
Illustrative product concept of an automated billet induction heating line

Illustrative product concept; final configuration is confirmed during engineering review.

FL-IH-PIP

Pipe & Plate Heating Line

In-line heating for pipe coating, bending, normalising and plate hot-forming, with continuous throughput and zone temperature control.

Read More →
Illustrative product concept of an automated billet induction heating line

Illustrative product concept; final configuration is confirmed during engineering review.

Tell us what your process needs.

Share the material or part, target output or treatment result, operating schedule and site utilities. Our engineers can review the equipment configuration and quotation scope against your application.