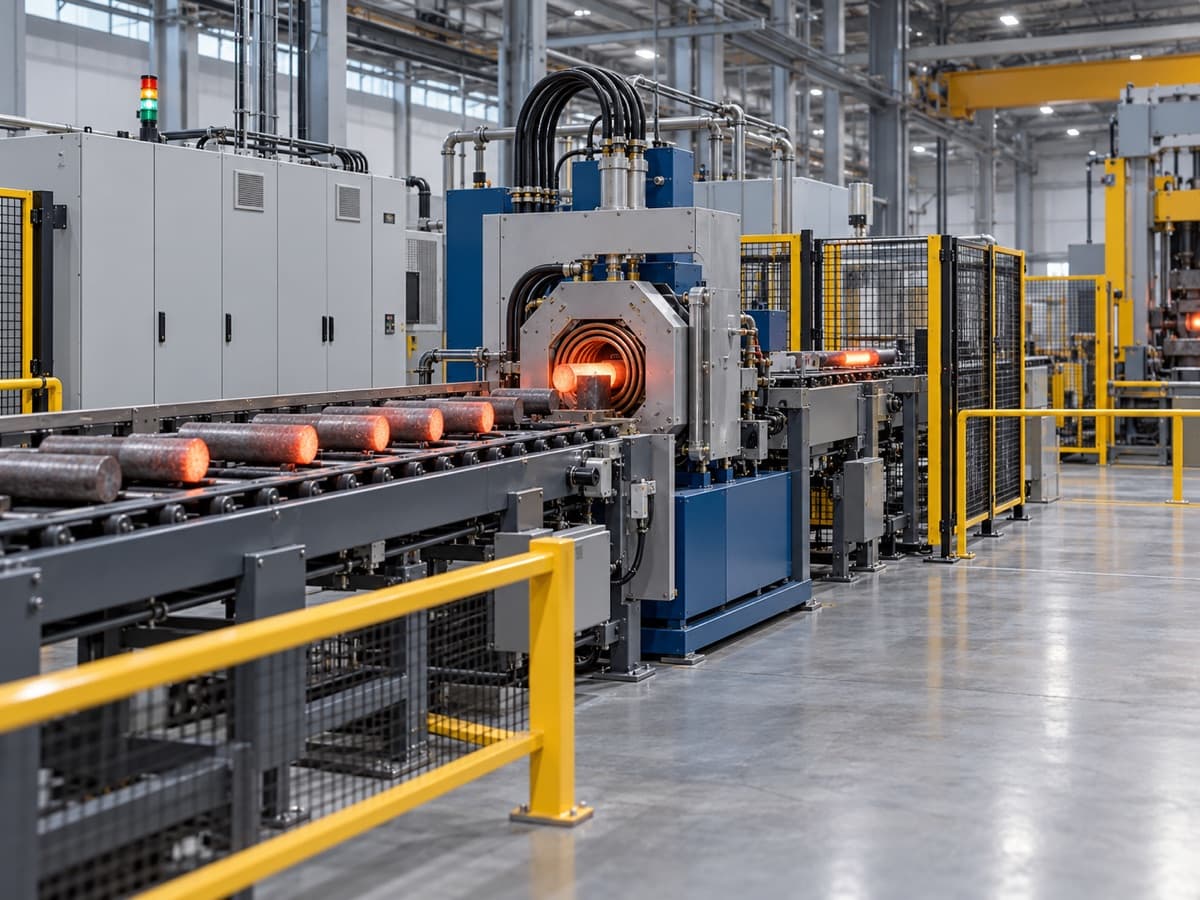
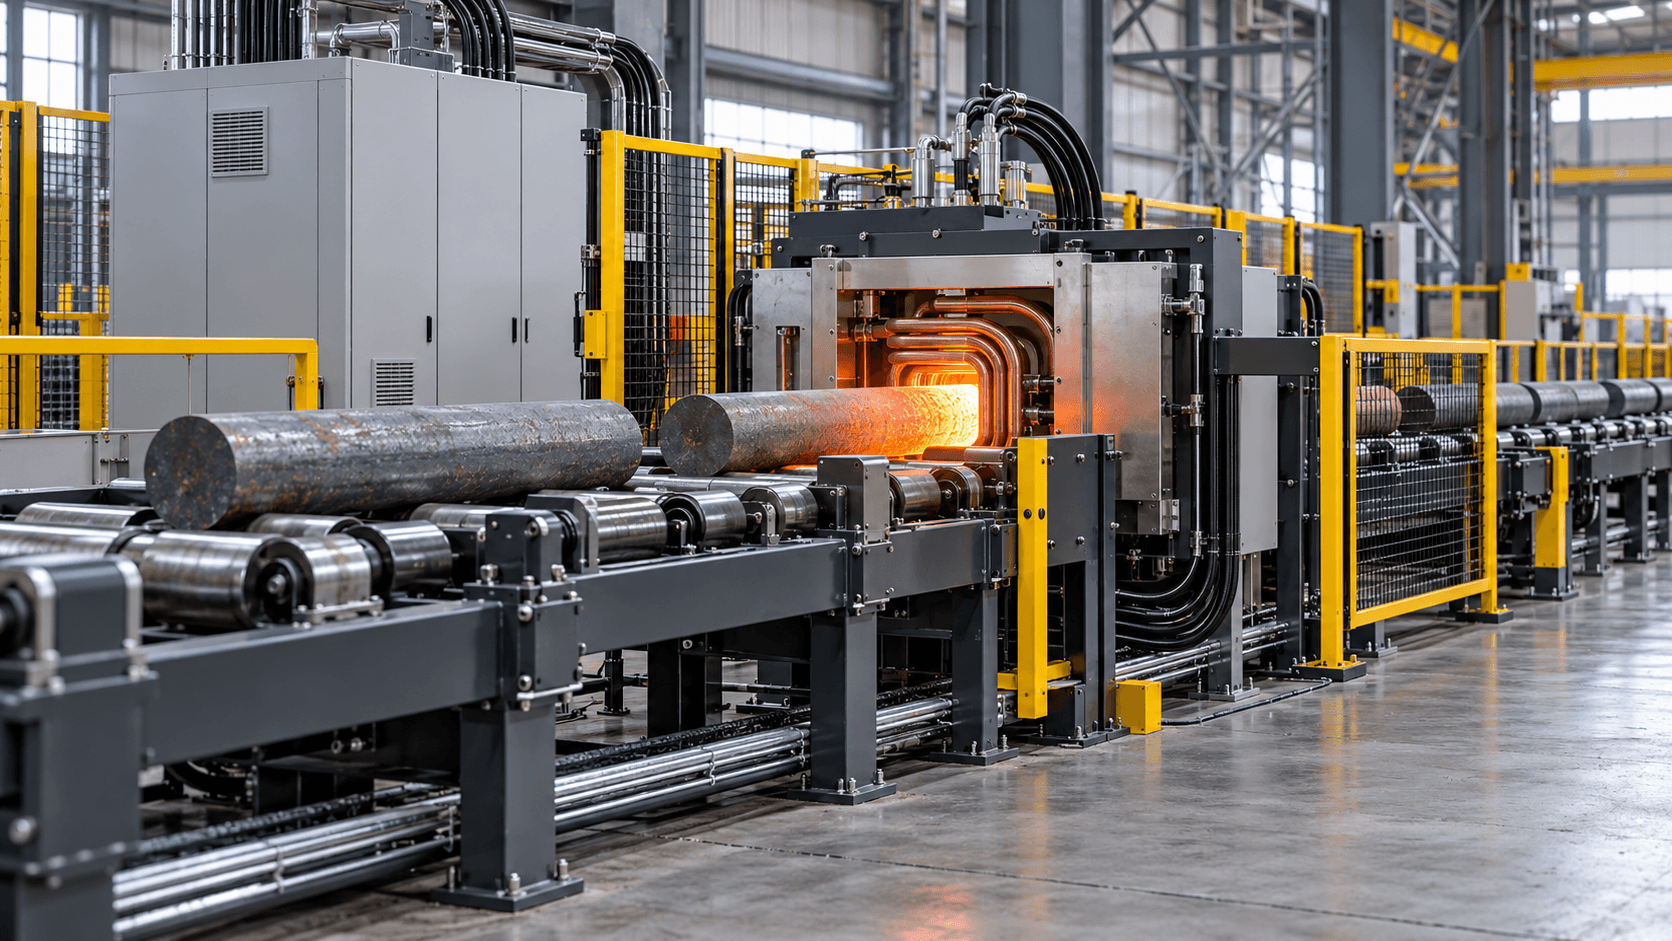
Pipe and plate lines heat continuously moving product rather than discrete parts, so the control problem is holding temperature against a varying line speed. Our lines use multi-zone coils with independent power control and a pyrometer at the exit of each zone.
Typical duties are pre-heating pipe before three-layer polyethylene coating, heating for induction bending, post-weld normalising of seam-welded tube, and heating plate before hot forming or levelling.
Coils are split-design so a line stoppage does not require the product to be stripped out, and the line integrates with the existing conveyor's speed signal so heating tracks throughput automatically.