FL-IH-BIL
GTR Billet Induction Heating Furnace
GTR series through-heating line for round and square billets, with pyrometer control, hot and cold reject gates and press synchronisation.
Read More →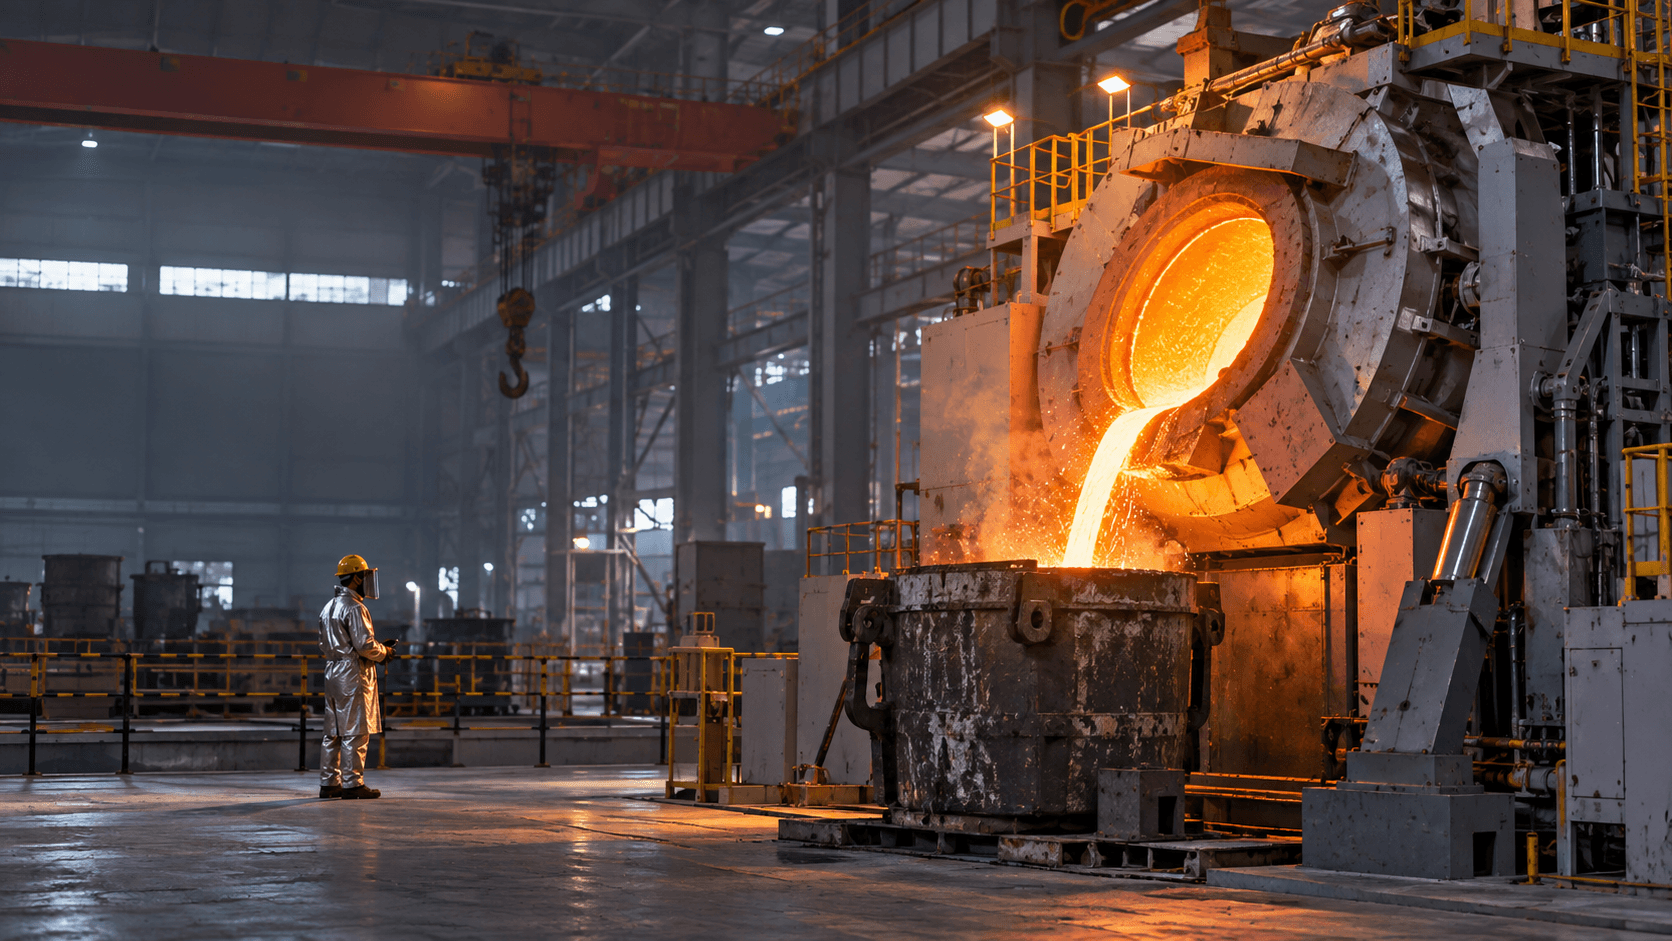
Induction heating manufacturer since 1998 · Built to your grid voltage · Installation & commissioning worldwide
Induction Heating Systems · FL-IH-QT
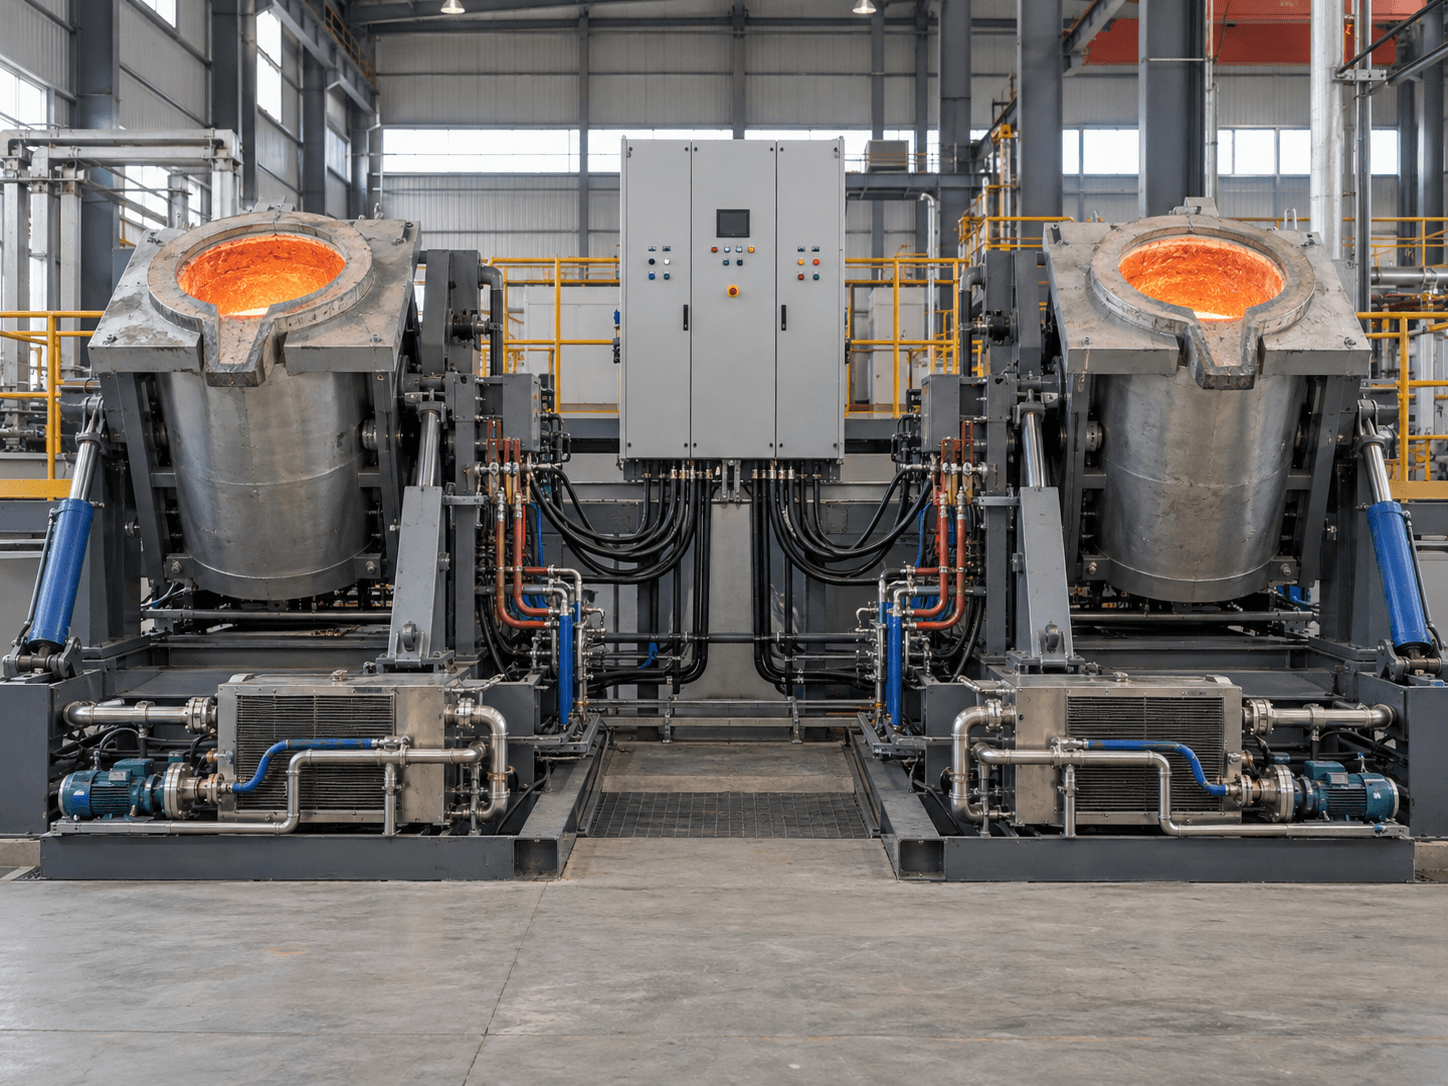
In-line hardening plus tempering in a single continuous pass — for steel strand, PC bar, drill rod, grinding rod and tube, with per-zone temperature control.
A quenching and tempering line does in one continuous pass what a batch furnace does in two separate shifts. Product runs through an austenitising coil, a quench box, then a tempering coil, emerging at final hardness without ever being stacked, cooled and reloaded.
The economics are what make it worth building: no work-in-progress inventory between hardening and tempering, no reheating from cold for the temper, and mechanical properties that repeat because every metre of product sees the same thermal cycle rather than a position in a batch.
These lines are specified for steel strand and PC bar production, where consistent tensile and relaxation properties along the full coil length are the whole specification. Line speed, coil count and quench design are set to your product and target properties.
FL-IH-BIL
GTR series through-heating line for round and square billets, with pyrometer control, hot and cold reject gates and press synchronisation.
Read More →FL-IH-END
Heats only the section to be formed — hand tools, axles, anchor bolts and eye bolts — cutting energy per part sharply versus full-length heating.
Read More →FL-IH-HRD
Scan or single-shot hardening with servo traverse, integrated quench and closed-loop power control — repeatable case depth on shafts, gears and rails.
Read More →FL-IH-PIP
In-line heating for pipe coating, bending, normalising and plate hot-forming, with continuous throughput and zone temperature control.
Read More →Send your alloy, target output per hour, working hours and grid voltage. You will get a capacity recommendation, a plant layout and a firm quotation — normally within three working days, no obligation.