Skip to content
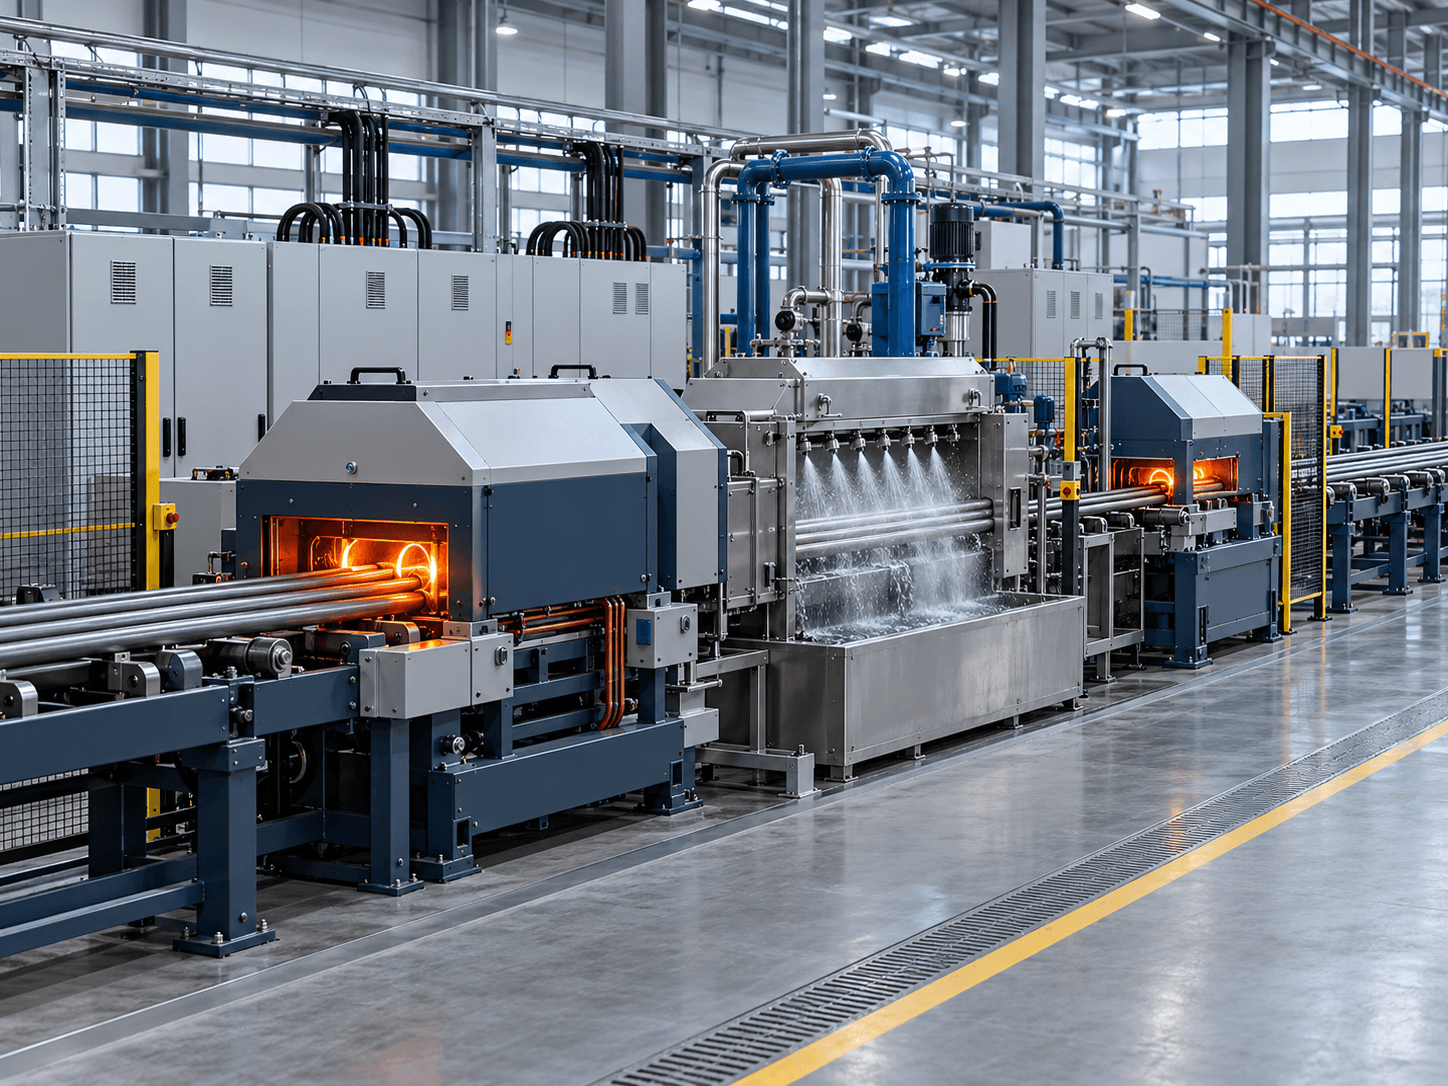
Continuous induction quenching, controlled water spray and tempering line for steel bar and strand

Illustrative product concept; final configuration and specifications are confirmed during engineering review.

Material & process

Share the workpiece alloy, dimensions and target process so the equipment route can be reviewed.

Output & duty

Define batch or throughput needs, operating schedule and required temperature or treatment result.

Site & utilities

Confirm available power, cooling, layout and destination-market requirements before final specification.

Induction Heat Treatment Systems · FL-IH-QT

Continuous Induction Quenching and Tempering Line for Bar, Strand and Tube

In-line hardening plus tempering in a single continuous pass — for steel strand, PC bar, drill rod, grinding rod and tube, with per-zone temperature control.

  • Hardening and tempering in one continuous pass — no intermediate handling
  • No work-in-progress inventory between the two heat treatments
  • Independent temperature control on the hardening and tempering zones
  • Consistent properties along the full product length, not batch-averaged
  • Continuous process data logging for customer property certificates
Product diameter
6 – 80 mm bar, strand or tube
Line speed
5 – 60 m / min, product dependent
Austenitising temperature
Up to 1,000 °C
Tempering temperature
350 – 650 °C, independently controlled
Quench
Water, polymer or oil, with flow and temperature control
Power supply
KGPS or IGBT, 100 – 3,000 kW total
Temperature control
Pyrometer closed loop per zone
Data
Continuous logging of temperature, speed and quench

Product Details

A quenching and tempering line does in one continuous pass what a batch furnace does in two separate shifts. Product runs through an austenitising coil, a quench box, then a tempering coil, emerging at final hardness without ever being stacked, cooled and reloaded.

The economics are what make it worth building: no work-in-progress inventory between hardening and tempering, no reheating from cold for the temper, and mechanical properties that repeat because every metre of product sees the same thermal cycle rather than a position in a batch.

These lines are specified for steel strand and PC bar production, where consistent tensile and relaxation properties along the full coil length are the whole specification. Line speed, coil count and quench design are set to your product and target properties.
FL-IH-HRD

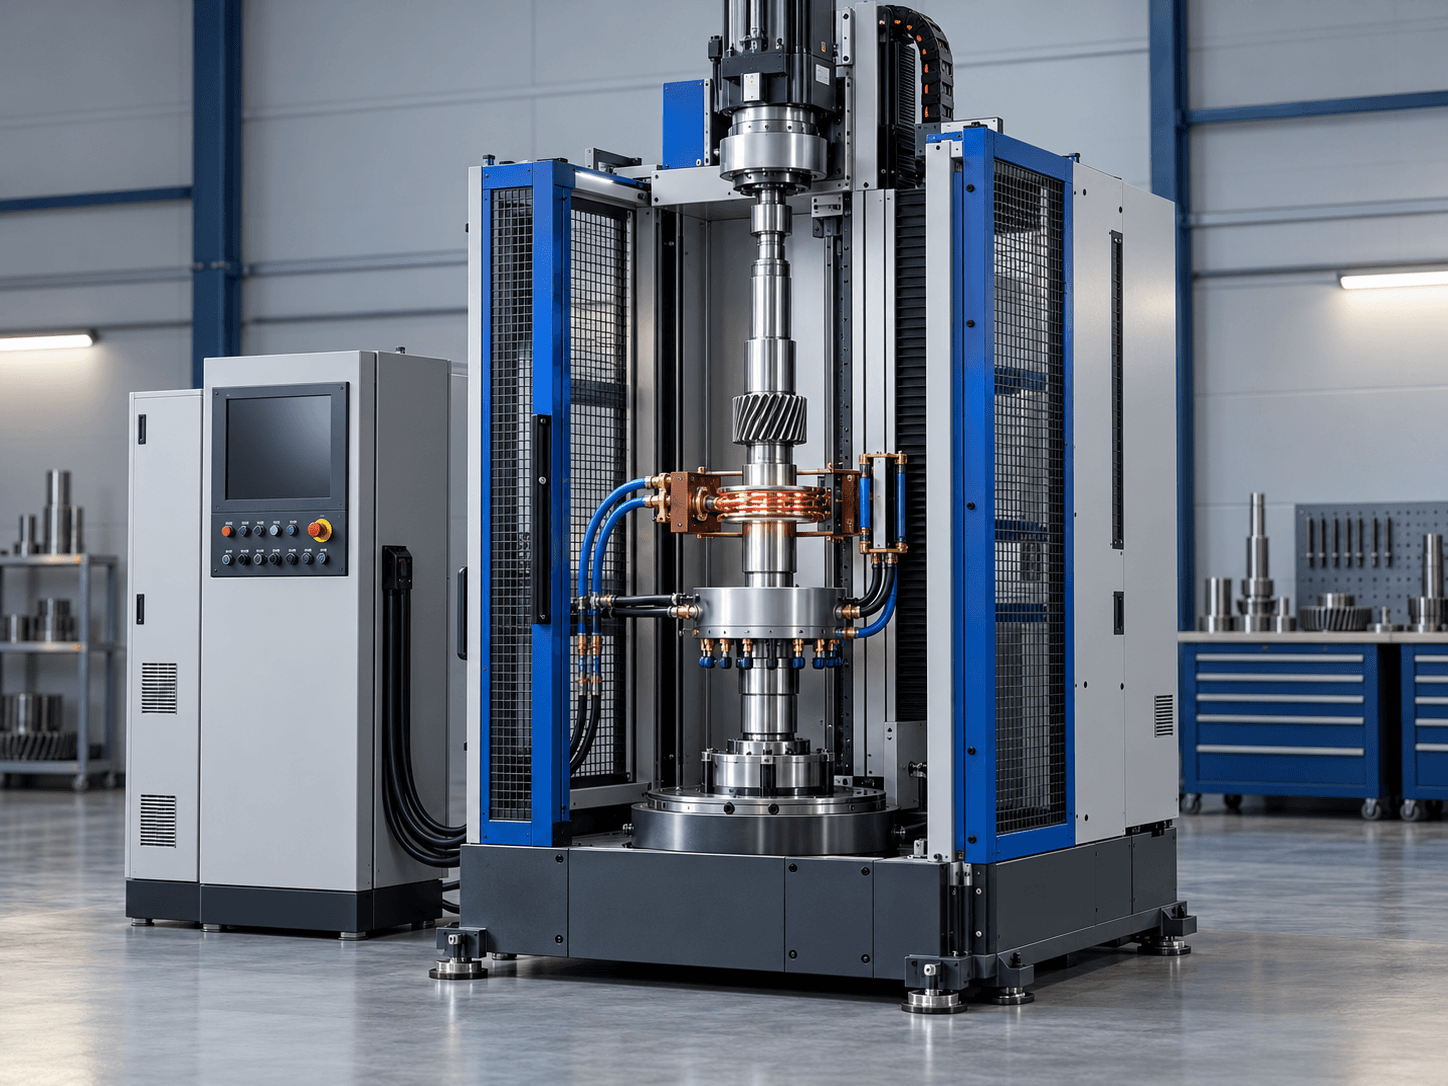
Induction Hardening Machine

CNC induction hardening configurations for shafts, gears, rails and other steel parts, engineered around part geometry, alloy, target case depth and line requirements.

Read More →
Illustrative product concept of a CNC induction hardening cell with a shaft, gear, induction coil and quench station

Illustrative product concept; final configuration is confirmed during engineering review.

Tell us what your process needs.

Share the material or part, target output or treatment result, operating schedule and site utilities. Our engineers can review the equipment configuration and quotation scope against your application.