Skip to content
Illustrative product concept of a steel-shell induction melting furnace in a foundry setting

Illustrative product concept; final configuration and specifications are confirmed during engineering review.

Material & process

Share the workpiece alloy, dimensions and target process so the equipment route can be reviewed.

Output & duty

Define batch or throughput needs, operating schedule and required temperature or treatment result.

Site & utilities

Confirm available power, cooling, layout and destination-market requirements before final specification.

Melting Furnaces · FL-HQ

Small Induction Melting Furnace for Laboratories and Investment Casting

Bench and floor-standing furnaces from 1 kg to 100 kg with fast heat-up and tight temperature control, for R&D, dental, jewellery and investment casting.

  • Closed-loop temperature control to ±3 °C
  • Rapid heat-up — minutes, not hours, between experiments
  • Optional argon purge chamber for reactive alloys
  • Tilting or lift-crucible pour, single-phase 220 V options below 25 kW
  • Programmable ramp-and-soak recipes with data logging
Capacity
1 kg – 100 kg
Rated power
15 – 100 kW
Frequency
2,500 – 20,000 Hz
Max temperature
1,700 °C
Temperature control
±3 °C, pyrometer or thermocouple feedback
Heat-up time
Minutes from cold on a 1 kg crucible
Atmosphere
Air, or argon purge chamber on request
Lead time
25 – 35 days

Product Details

Small induction furnaces are specified for repeatability rather than throughput. The HQ series holds set-point within ±3 °C and reaches 1,600 °C from cold in a few minutes on a 1 kg crucible, which is what a metallurgy laboratory or an investment casting shop needs between pours.

Configurations include open-air melting, controlled atmosphere with an argon purge chamber, and tilting or lift-crucible pouring. Optical pyrometer or immersion thermocouple feedback drives closed-loop temperature control.

Common users are university metallurgy departments, alloy development labs, jewellery and dental casters, and investment casting shops pouring small-batch superalloy or stainless components.
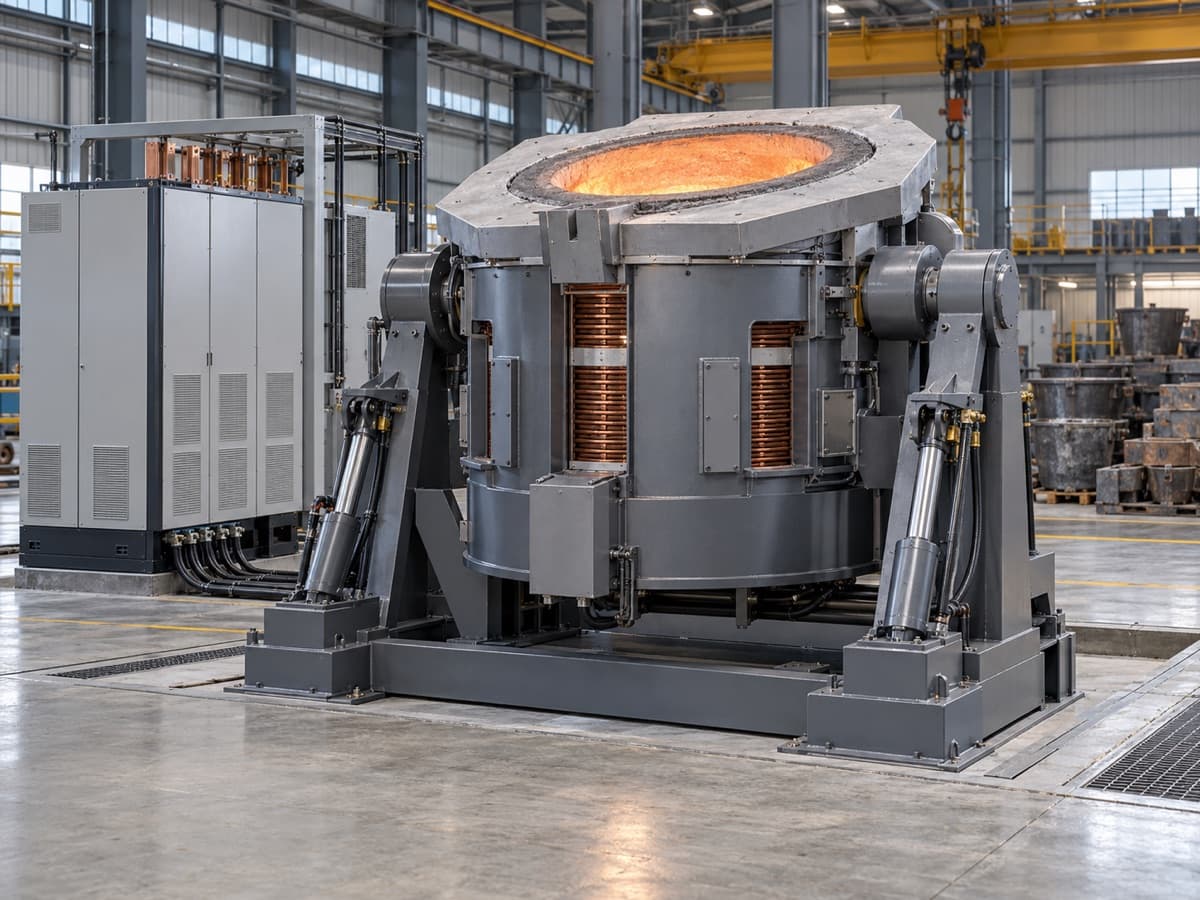
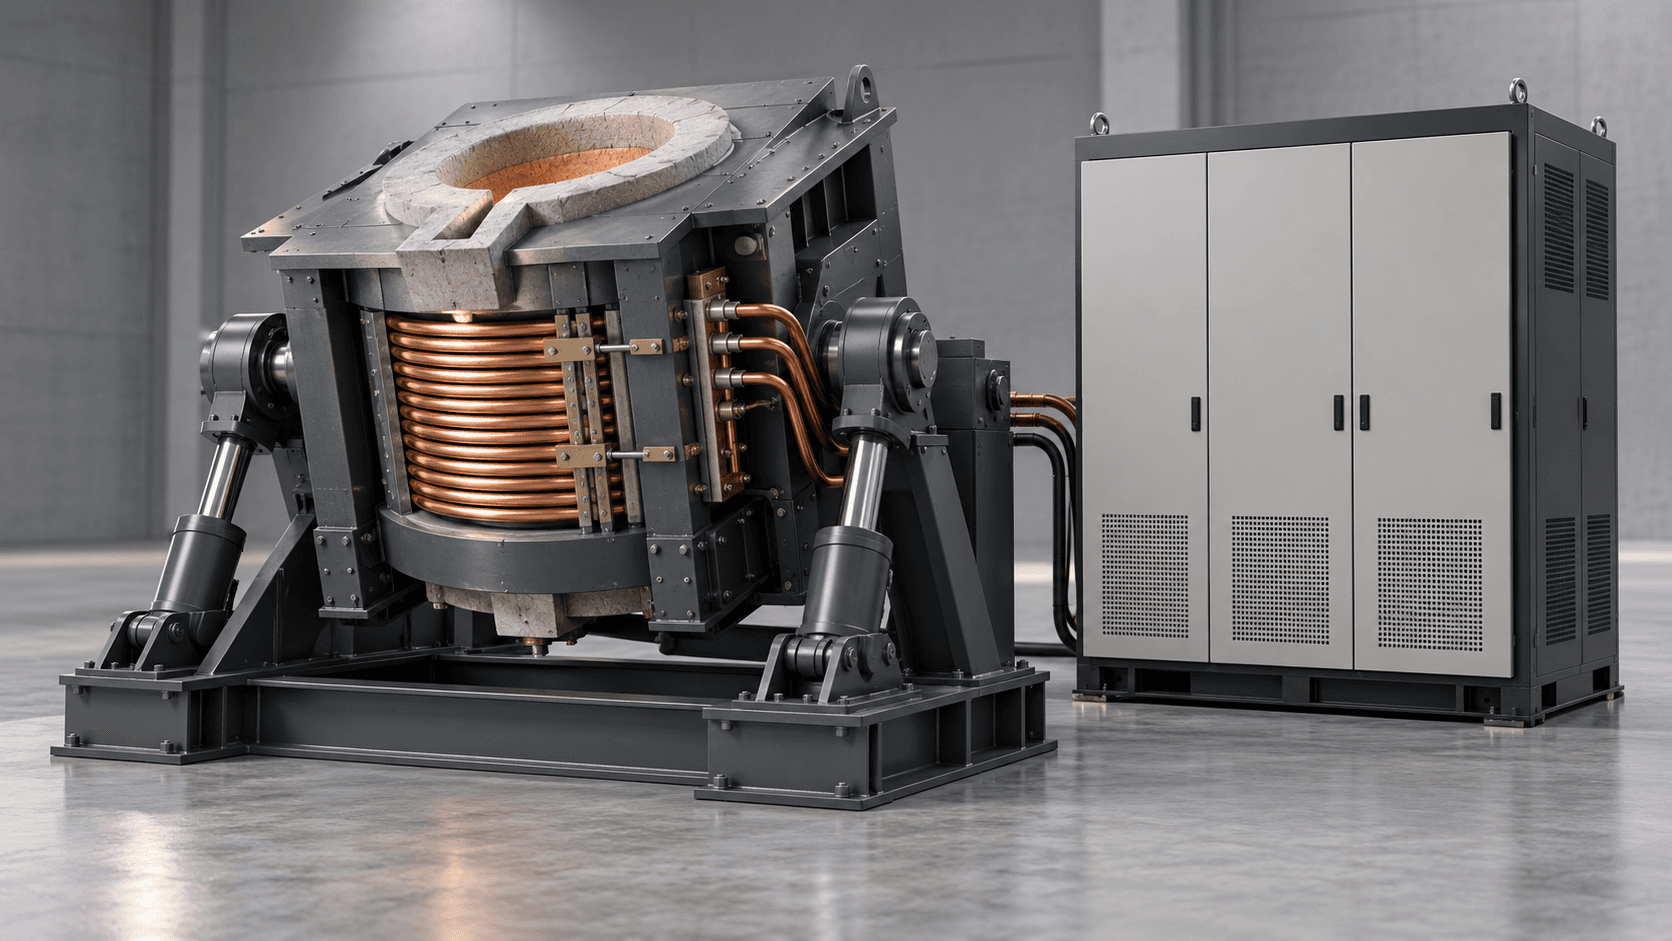
FL-GW-SS

Steel Shell Induction Melting Furnace

Fully welded steel-shell furnace with magnetic yoke and hydraulic 95° tilting, from 0.5 to 5 tons per body — the standard choice for continuous foundry melting.

Read More →
Studio product visualization of a steel-shell induction melting furnace and power cabinet

Illustrative product concept; final configuration is confirmed during engineering review.

FL-GW-AS

Aluminium Shell Induction Melting Furnace

Lightweight aluminium-frame furnace for small and medium foundries — lower installed cost, faster relining, ideal below 3 tons.

Read More →
Illustrative product concept of a steel-shell induction melting furnace in a foundry setting

Illustrative product concept; final configuration is confirmed during engineering review.

FL-GW-DT

Dual-Track Melting Furnace System

Two furnace bodies sharing a single medium frequency power supply, switched from one console so melting never stops for a lining change.

Read More →
Illustrative product concept of a steel-shell induction melting furnace in a foundry setting

Illustrative product concept; final configuration is confirmed during engineering review.

FL-GWL

Aluminium Melting & Holding Furnace

Low-frequency induction furnace tuned for aluminium and its alloys, with gentle stirring, low burn-off and a holding mode for die-casting lines.

Read More →
Illustrative product concept of a steel-shell induction melting furnace in a foundry setting

Illustrative product concept; final configuration is confirmed during engineering review.

Tell us what your process needs.

Share the material or part, target output or treatment result, operating schedule and site utilities. Our engineers can review the equipment configuration and quotation scope against your application.