Skip to content
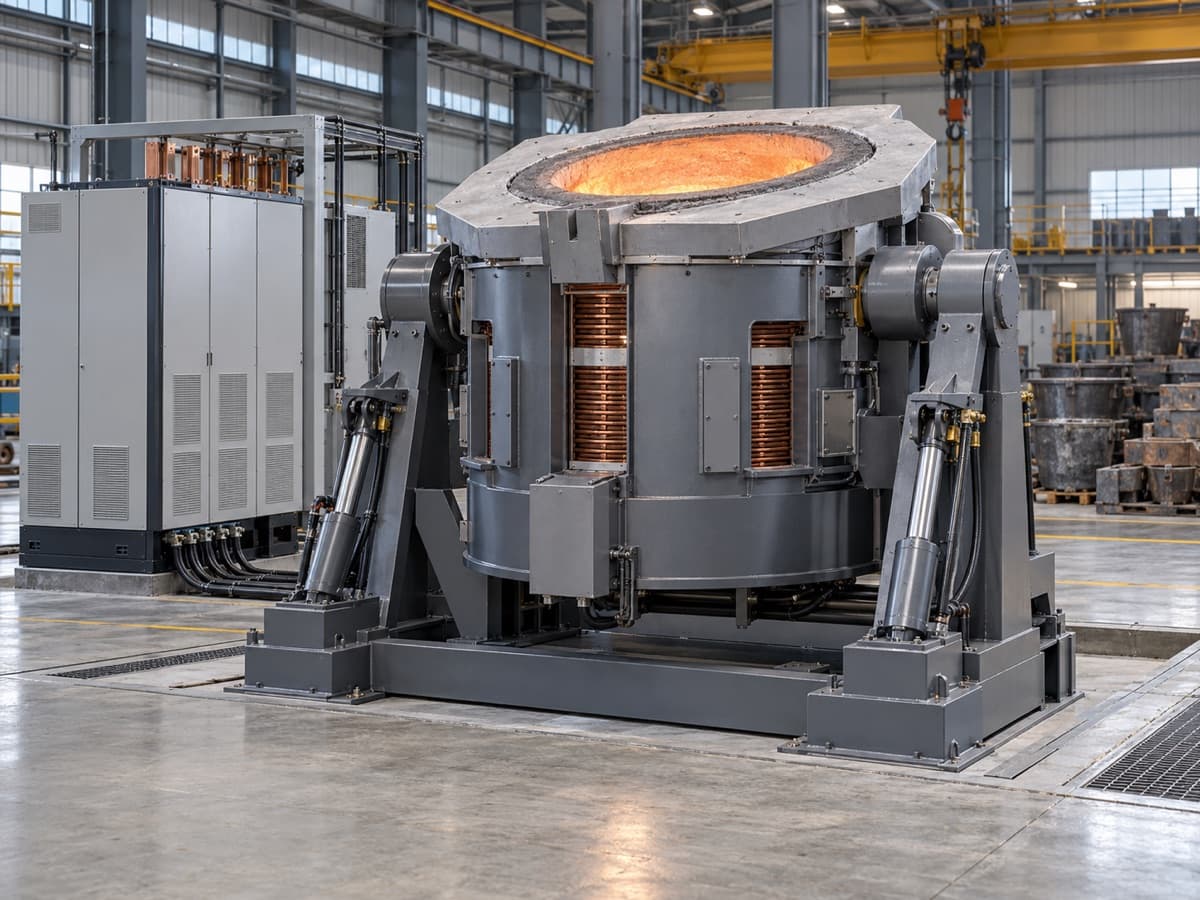
Illustrative product concept of a steel-shell induction melting furnace in a foundry setting

Illustrative product concept; final configuration and specifications are confirmed during engineering review.

Material & process

Share the workpiece alloy, dimensions and target process so the equipment route can be reviewed.

Output & duty

Define batch or throughput needs, operating schedule and required temperature or treatment result.

Site & utilities

Confirm available power, cooling, layout and destination-market requirements before final specification.

Melting Furnaces · FL-GW-DT

One Power Supply, Two Furnace Bodies — Dual-Track Melting System

Two furnace bodies sharing a single medium frequency power supply, switched from one console so melting never stops for a lining change.

  • No production stop for relining — melt on one body, reline the other
  • Higher return on the power supply investment
  • Electrically and hydraulically interlocked for safe maintenance
  • Optional different capacities on the two bodies (e.g. 3 t + 1 t)
  • Single console — no extra operator required
Configuration
1 power supply + 2 furnace bodies
Capacity
0.5 – 5 t per body, larger to order
Switching
Interlocked vacuum contactor cabinet
Changeover time
Under 2 minutes
Tilting
Independent hydraulic station per body
Control
Single operator console with body selector
Lead time
50 – 80 days
Warranty
12 months

Product Details

In a dual-track system a single power supply feeds two furnace bodies through a switching cabinet. One body melts and pours while the other cools, is relined or is held on standby. Utilisation of the power supply — the most expensive item in the plant — goes up, and the lining change stops being a production shutdown.

The switching cabinet is interlocked so power can only be applied to one body at a time, and the water and hydraulic circuits are separately valved so work on the idle body is safe while the other is at full power.

This is the configuration we supply for most foundries running two or three shifts. It costs more than a single-body furnace of the same capacity, and on a two-shift operation the avoided relining downtime usually recovers the difference inside the first year.
FL-GW-SS

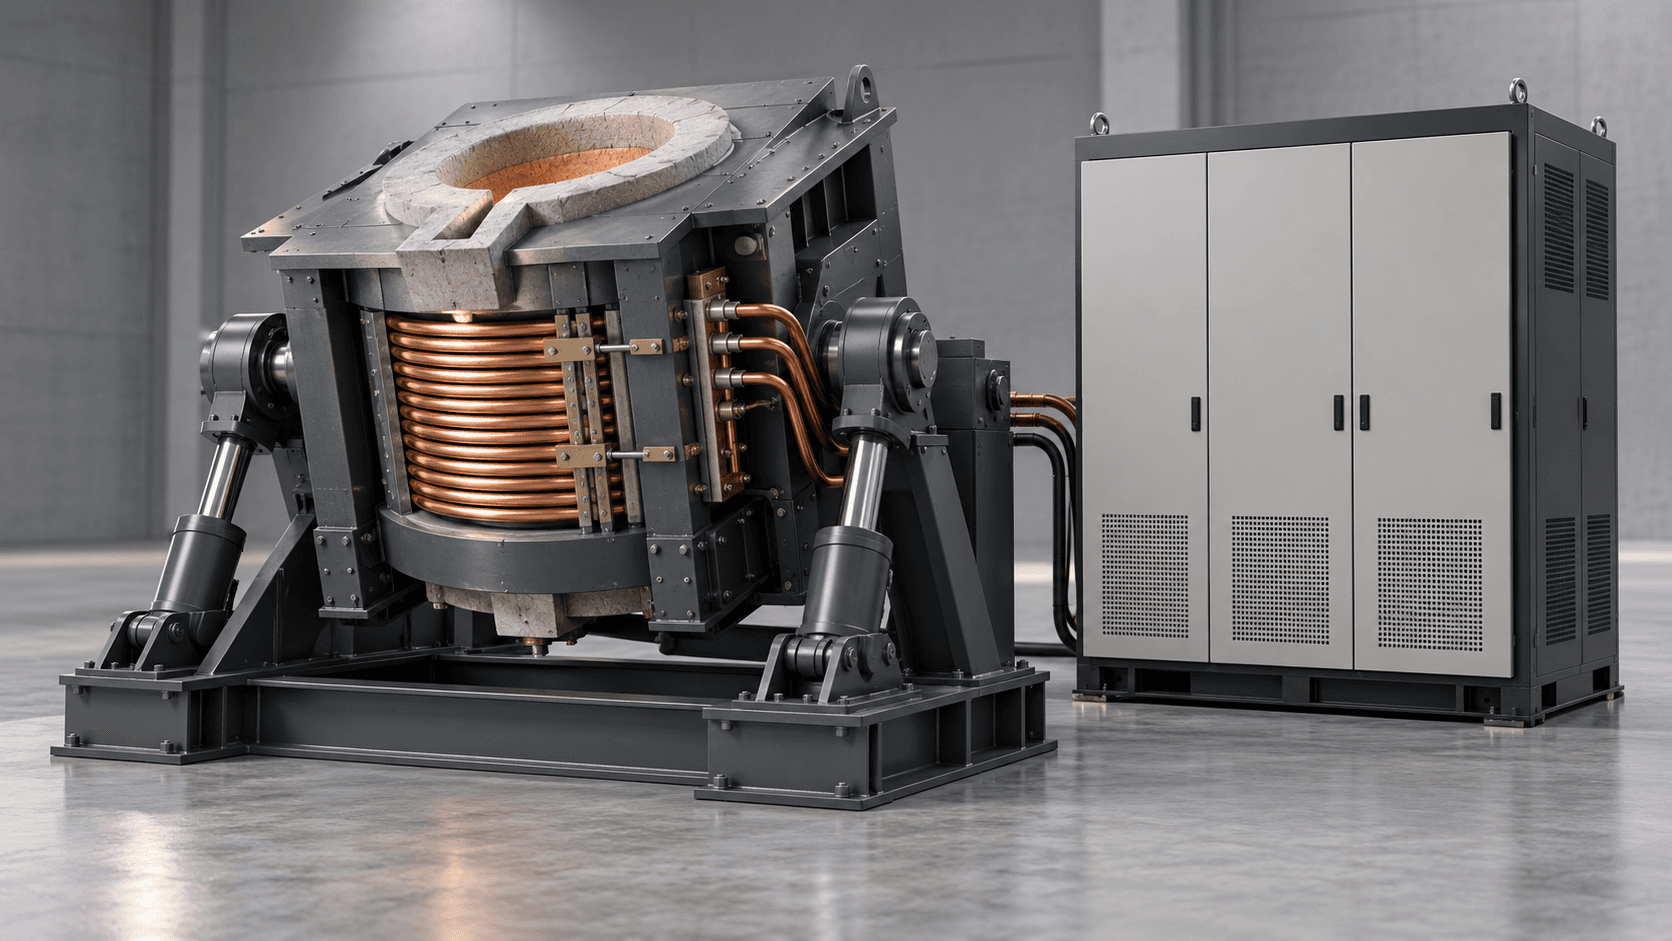
Steel Shell Induction Melting Furnace

Fully welded steel-shell furnace with magnetic yoke and hydraulic 95° tilting, from 0.5 to 5 tons per body — the standard choice for continuous foundry melting.

Read More →
Studio product visualization of a steel-shell induction melting furnace and power cabinet

Illustrative product concept; final configuration is confirmed during engineering review.

FL-GW-AS

Aluminium Shell Induction Melting Furnace

Lightweight aluminium-frame furnace for small and medium foundries — lower installed cost, faster relining, ideal below 3 tons.

Read More →
Illustrative product concept of a steel-shell induction melting furnace in a foundry setting

Illustrative product concept; final configuration is confirmed during engineering review.

FL-GWL

Aluminium Melting & Holding Furnace

Low-frequency induction furnace tuned for aluminium and its alloys, with gentle stirring, low burn-off and a holding mode for die-casting lines.

Read More →
Illustrative product concept of a steel-shell induction melting furnace in a foundry setting

Illustrative product concept; final configuration is confirmed during engineering review.

FL-GWT

Copper & Brass Melting Furnace

Medium frequency furnace for copper, brass and bronze with zinc-vapour extraction and tilting pour, sized 100 kg to 10 tons.

Read More →
Illustrative product concept of a steel-shell induction melting furnace in a foundry setting

Illustrative product concept; final configuration is confirmed during engineering review.

Tell us what your process needs.

Share the material or part, target output or treatment result, operating schedule and site utilities. Our engineers can review the equipment configuration and quotation scope against your application.